Thermo-Cognitive Advanced Process Control (TC-APC) models, simulates and optimizes your process in real time to improve yield, conversion and throughput, and reduce energy use, with a quick payback.
Aroma and specialty chemicals, batch and continuous
How much prime product is in your intermediate cut?
Probably more than anyone thinks. It has nothing to do with the operator's skill and everything to do with the instrument he steers by:
Temperature at the column head.
It moves with pressure as much as it moves with composition, and it is least trustworthy exactly when it matters most: adjust the reflux to sharpen the cut and the reading takes time to catch up with what the column is actually doing.
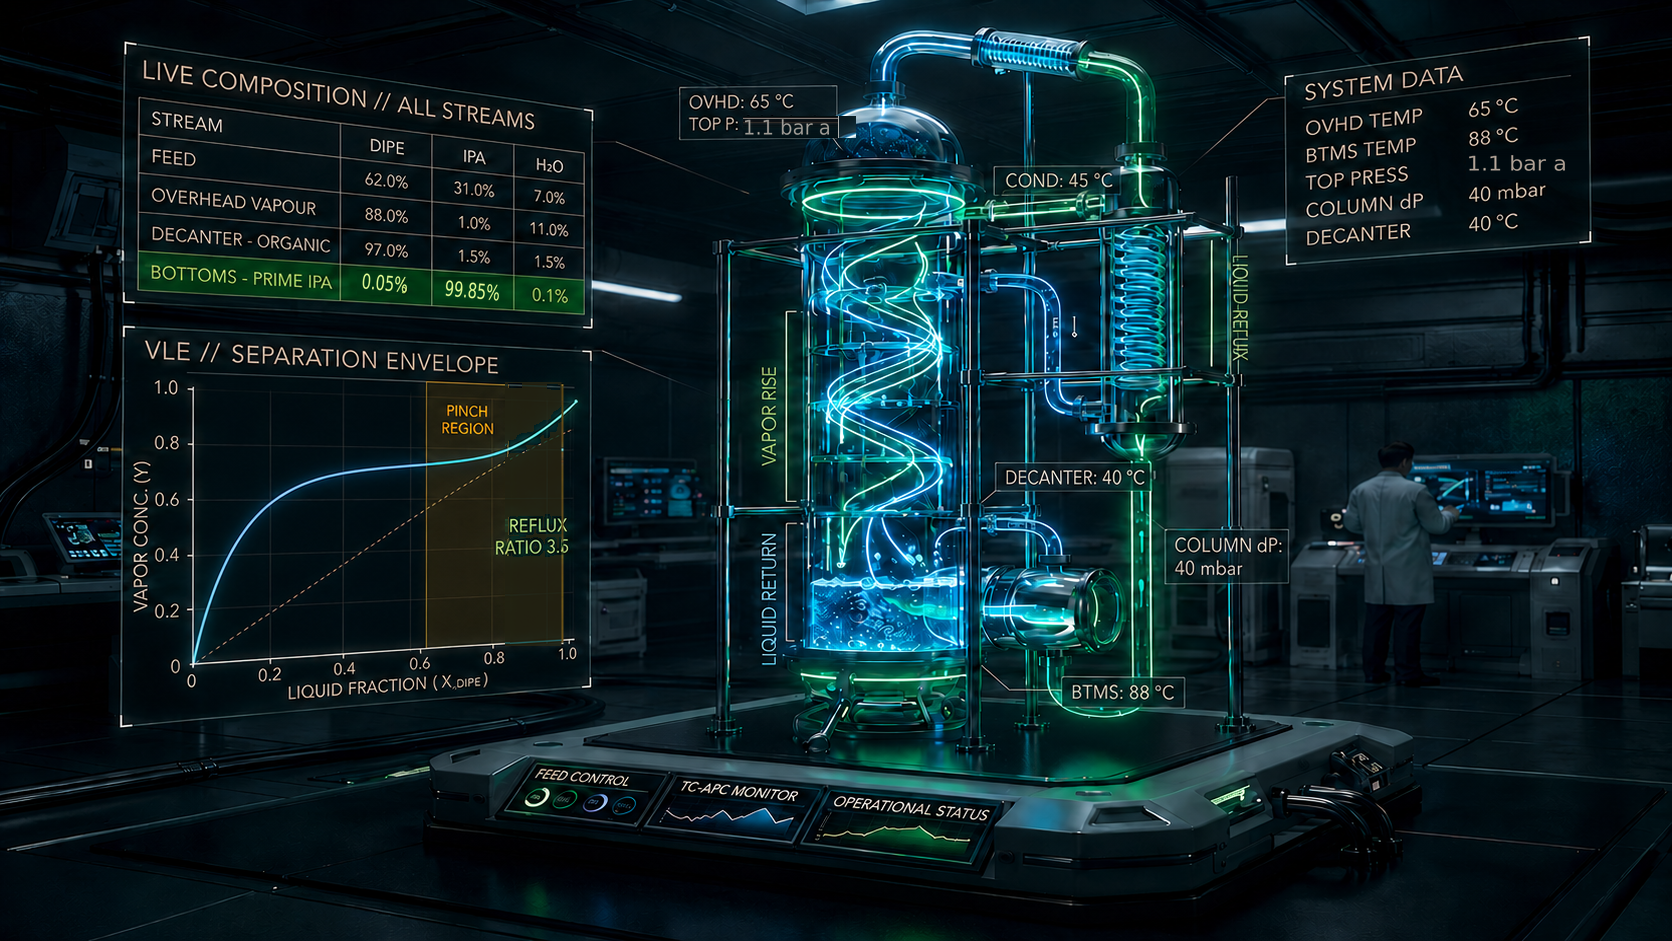
What the engine sees, drawn as if the column were transparent. Representative column, indicative values. The panels show live composition on feed, overhead, decanter and bottoms, the separation envelope with the pinch region marked, and the column's operating temperatures, pressure and differential pressure.
Published analysis. Begins with a data audit on one column.
The science under TC-APC
A column's result is decided in the vapor and the liquid.
Which compounds leave at the head, and when, is settled between the vapor and the liquid on every tray, not by the temperature read at the top. That's the science TC-APC is built on, and AI makes it sharper.
Three moments decide the batch.
Fore-run to main cut, main cut to intermediate, intermediate to residue. The periods between them are largely a matter of holding conditions steady. Almost all of the yield is settled in those three decisions.
The operator making them has a head temperature, one or two tray temperatures, a column pressure, a distillate rate, and a gas chromatograph result that arrives every thirty to forty minutes. The specification he is working to is usually odor and color rather than assay, and a batch can pass on GC while failing on the nose.
So the decision that determines the yield is taken on a temperature and an intermittent laboratory result, against a specification that neither of them measures.
Before you read any further, test it
Assay the intermediate cut. If it holds a significant fraction of prime product, the bias is real and its size is measurable from your own mass balance.
If it does not, your column is already being run close to its limit and there is nothing here worth pursuing. We would rather you found that out from a laboratory sample than from a meeting.
Worth counting twice, because it costs twice. Once as prime product that left in the wrong drum, and again as the kettle hours spent pooling and reboiling it, which are hours that vessel could not spend on a fresh charge.
Batch fractionation
The column at the end of the batch is not the column your loops were tuned for.
A batch column is a draining system. As the still depletes, the same reflux move does something different at the end of the batch than it did at the start. A loop tuned to be responsive early will hunt late, so it is detuned until it is sluggish enough to survive the end of the run, and the reflux target is set high enough to be safe in the worst minute of the batch.
That margin is then carried for the whole batch, not just for the minute it was chosen for.
And the loop that trims it is steering on a signal that cannot resolve a cut.
Your reflux is not a fixed number. It is trimmed to hold head temperature, which is why it moves. Under vacuum, head temperature moves with pressure as much as it moves with composition. A three millibar drift, a condenser fouling slightly, a gland leaking, a vacuum pump warming through the shift, moves the apparent boiling point by four to six degrees.
So when the vacuum wanders, the loop reads a composition change that did not happen and moves the reflux to correct it. The loop is not idle. It is working hard, and faithfully, on a false signal.
When the noise from pressure is wider than the transition you are trying to detect, the temperature reading cannot resolve the cut.
The operator is not guessing badly. He is guessing.
What the margin costs, besides steam
You are not getting the stages you paid for. Heavy liquid loading thickens the film running down the packing and encourages channeling and maldistribution. The bed is physically unchanged and separating as though it had fewer stages than the one you bought. The defensive reflux that keeps the loop calm is part of what takes them away.
And the molecule is sitting in the heat for longer. A higher reflux means more boil-up, a longer batch and more hours at temperature for material that does not enjoy being hot. In an odor-critical product that is not only a yield question. It is the difference between a bright top note and a flat one, and it does not show up on an assay.
Both are visible in your own records. Compare the separation you are achieving against what the bed was specified for, and compare the batch length you are running against the one the process was designed around.
The movement in the flat line is the loop answering a pressure drift as though it were a composition change. The height of it is the margin that keeps the loop stable as the still depletes, chosen for the worst minute of the batch and carried for all of them.
And it is still short at the end, where the cut is made and where more reflux is what the separation actually needs.
You already know what is in the feed. You start the batch the same way regardless.
Natural feedstocks vary, and the isomer ratio in turpentine differs by origin and by season. Most plants analyze every incoming lot, file the certificate, and then run the standard recipe. That assay is a feed-forward signal you have already paid for, and it can be used to position the column before the batch starts rather than discovering the difference partway through it.
Continuous fractionation
The same signal, failing in a different place.
On a continuous column the composition is still inferred from a temperature, and near a pinch that temperature goes flat exactly where the cut point sits. A real shift in composition produces almost no change in the reading. The signal disappears precisely where you need it.
Meanwhile the feed rate, the upstream conversion and the steam header pressure all move during ordinary operation. Fixed gain loops answer each of those separately, with no model of how reflux, boil-up and column pressure interact with one another. A drop in the header sends the steam valve hunting; the column answers with vapor waves; the operator raises internal traffic to keep the heavy component out of the bottoms, and prime product goes overhead with it.
With no composition signal to trust, the only safe answer is margin. And that margin is carried permanently, not only during the upset that justified it.
The difference
Your DCS is not doing anything wrong.
It holds temperature, pressure and flow precisely, which is exactly what regulatory control is built to do. It has no composition to hold, because nothing measures composition. TC-APC gives it one, and writes setpoints back to it.
| Today | With TC-APC | |
|---|---|---|
| Composition | Inferred from head temperature, confirmed by GC every thirty to forty minutes | Estimated continuously, with the last GC result and the running bias shown beside it |
| Pressure drift | Enters the temperature reading as a composition change, and the loop acts on it | Measured and accounted for, so a pressure move is not read as a composition move |
| The cut | Operator judgment against a signal that cannot resolve it | Held at the cut point, with the reason for every move shown on the screen |
| Reflux | Trimmed to hold a head temperature, on a plateau set for the worst minute of the batch | Moved through the batch against the estimated composition as the still depletes |
| Loop tuning | Set once and detuned enough to survive the end of the run | Re-solved continuously as the column changes through the batch |
| Incoming lot | Assayed, filed, and not used | Used to position the column before the batch begins |
| When something drifts | The operator notices, or the laboratory does | The bias against your own GC is already on the screen |
| The cut decision | Rests with whichever operator is on shift | Made the same way on every batch, and recorded with the model state that produced it |
What arrives on site
A system, not a report.

- SystemIndustrial fanless unit, rack or panel mounted, running the thermodynamic model and the optimizer.
- Operator HMIField panel showing the live estimate, the last lab result, the current bias and the reason for every move.
- InterfaceOPC‑UA or Modbus to your existing DCS, PLC or SLC. Reads process variables, writes setpoints. No change to your control system.
- GuardrailsHeartbeat watchdog and rate‑of‑change limits held in the DCS block. On any timeout, implausible estimate or out‑of‑range output, control reverts to the DCS with bumpless transfer to predefined fallback setpoints.
- Before it writesTuned offsite against a simulator, then run on your column in shadow mode until the estimate tracks your GC inside a tolerance you set.
What this cannot do.
It cannot loosen an odor specification
Odor-active minor components enter the objective function as hard constraints, never as terms to be traded against yield. A scheme that improves recovery by relaxing an impurity limit has not solved the problem. It has moved it to your customer.
It cannot defeat a phase equilibrium
Where a separation is capped by an azeotrope, no control policy changes that. The answer there is a different separation, not better control of this one.
It cannot fix an under-staged or flooding column
If the stages are not there, a good estimator will report accurately that they are not there. That is worth knowing, and it is not a yield improvement.
It does not replace your gas chromatograph
It interpolates between GC results and holds the column steady in between. The GC remains the reference and the arbiter, and the bias between the two is on the screen.
And one commercial caution that matters more than any of those
In flavor and fragrance your material is approved against a reference sample. Any change in cut policy that shifts the impurity profile, even in a direction that looks like an improvement, can trigger requalification.
So the first objective in this work should be reduced batch-to-batch variation, not increased yield. Consistency is what your customer actually pays for, it is the easier internal case to make, and the recovery tends to follow anyway as a consequence of running closer to a well characterized optimum.
The mark
Find the optimum. Hold it while it moves.
The curve is a yield or selectivity response. The amber point is the optimum, and the dashed drop is where it sits on the operating axis.
The second half of the line is the part that matters. Finding an optimum is a study, and studies end up in drawers. Holding one while the feed, the fouling, the weather and the wear keep moving it is a control problem, and that is the work.
Start with the note
Cut-point determination in the vacuum fractionation of odour-critical products
Three pages on the measurement problem and what can be inferred without new analyzers. Free, and nothing to sit through. No form, and we do not ask for your email address.
Or start with your column
Send three months of operating data from one column
We will tell you what your transition cut is costing you, with the uncertainty stated openly rather than buried. No charge, and no commitment either way. Including the answer that there is nothing here worth pursuing, if that is what your numbers say.
projects@yielddynamics.in Talk to IIT Bombay engineers Call +91 94230 07004Monday to Saturday, 9:00 to 19:00 IST