Thermo-Cognitive Advanced Process Control (TC-APC) models, simulates and optimizes your process in real time to improve yield, conversion and throughput, and reduce energy use, with a quick payback.
An invitation to system integrators
The optimum moves. Your setpoints don't.
TC-APC, Thermo-Cognitive Advanced Process Control, is an optimization layer above the DCS, PLC or single loop controller (SLC) you install. It finds the optimum as feed, load and weather change, and writes the setpoints in real time. Nothing you built is replaced.
Become a TC-APC Solution Partner, and offer it on the plants you have already commissioned.
Talk to IIT Bombay engineers Call +91 94230 07004Monday to Saturday, 9:00 to 19:00 IST
Where it sits
Commissioned once. Optimized in real time.
What arrives on site
A system beside the one you built, and nothing rewired.

- SystemIndustrial fanless unit, rack or panel mounted, running on its own machine alongside your controls. Your existing logic is not modified.
- Operator HMIField panel showing the live estimate, the last laboratory result, the current bias, and the reason for every move. Enclosure to suit the area.
- InterfaceOPC‑UA or Modbus to your existing DCS, PLC or SLC. Reads process variables, writes setpoints. Read-only through shadow mode and validation.
- InstallationMinimal wiring and no shutdown. In most plants the physical work is a day, and the schedule is set by the shadow-mode period rather than by the installation.
- What stays with the plantThe validated model. It remains useful for debottlenecking, operator training, what‑if studies and turnaround planning, whether or not TC-APC is writing.
Where it applies
You wired every instrument in the plant. The number that decides its money is not on any of them.
The instrument changes with the industry. The argument does not.
- Dryers, milk and chemical powders Outlet temperature tells you the air is hot. It does not tell you how wet the powder is.
- Aroma and specialty distillation A boiling point tells you something is boiling. It does not tell you what.
- Natural extracts and oleoresins A residual solvent result tells you the extract passed. It does not tell you what it lost to pass.
- Solvent recovery, DMSO and DMF The solvent is back in the tank. How much went to residue, and how much decomposed on the way, appears in no reading.
- IPA and DIPE separation Near the azeotrope the temperature goes flat exactly where the cut point sits. The signal disappears precisely where you need it.
- Sugar crystallization in vacuum pans Supersaturation decides the crystal. In seventy years nobody has measured it online.
- Soda ash carbonation The conversion is known when the analysis comes back. By then the tower has moved on.
- Boilers and combustion An oxygen reading tells you the excess air is right for the coal you assumed you were burning.
- Reaction selectivity, nitration and Grignard Temperature buys conversion and hazard in the same movement. Nothing tells you which one you have just bought.
- Any other process If a number nobody measures decides the money, the argument is the same.
What TC-APC is
Thermo for the physics. Cognitive for the plant.
Thermo, because it starts from the thermodynamics of the process: the balances and equilibria every unit obeys, whether anyone measures them or not. Cognitive, because it then learns from each plant what physics alone cannot know: how this unit fouls, how this feed varies, how this plant answers a move. Advanced Process Control, because what it does with both is decide the setpoints and write them, in real time, inside the limits the plant already has.
Why become a Solution Partner
Your best new client is a plant you've already commissioned.
A second sale on plants you know
You commissioned the DCS, PLC or SLC, you know the tags, and the plant already trusts you. TC-APC turns that installed base into new orders, with no new client to find.
Real equipment to install
A TC-APC system, rack or panel mounted, wired in beside the system you built.
A reason to stay after handover
Handover is usually the last visit. With TC-APC the plant sees the gain on its own meters, month after month, on a system you installed.
Tenders won on results
Most automation tenders are decided on price. A bid with TC-APC competes on what the plant gets back: yield, throughput and fuel.
Your side, our side
You know the plant. We know the physics.
Your side
- The client, and the relationship with it
- Site access, and the people on site
- Integration with the DCS, PLC or SLC
- The tag list
- Installing and wiring the TC-APC system
- Commissioning
Our side
- The data audit
- Customizing and tuning TC-APC to the process, offsite
- Fine-tuning on site, through shadow mode and validation
- Measuring the gain, on the plant's own meters
- Engineering backup for your team
How a Solution Partner project runs
Six steps, from a first conversation to setpoints written in real time.
01
We talk
What TC-APC is, and whether it fits your clients.
02
You bring a plant you know
One unit at one client, where a number nobody measures decides the money.
03
The data audit
Operating data from that unit, with the laboratory results beside it. We say how wide the margin is and what it is worth. If there is nothing worth pursuing, we say so.
04
Tuned offsite, then validated on site
TC-APC's model, simulation and optimization engines are built in. We customize and tune them to the process offsite, before the system arrives. On site, it first runs in shadow mode until its estimate matches the plant's own laboratory.
05
It writes the setpoints, in real time
From then on TC-APC writes the setpoints in real time, in small steps, inside limits held in the plant's own DCS, PLC or SLC. The operators see every move and the reason for it.
06
The gain, on the plant's own meters
Before and after, on the plant's own instruments, so the result is your client's to check.
What it never touches
The DCS obeys. TC-APC decides.
It decides the setpoints and nothing else. Everything that keeps the plant safe stays where you put it.
- Safety logic. Burner management, interlocks, trips and any other safety logic. TC-APC writes nothing into them and cannot.
- The limits. Rate-of-change clamps, the watchdog and the fallback setpoints are configured in the client's DCS, PLC or SLC, by your engineers or the client's. TC-APC cannot alter them.
- Bumpless fallback. If the link drops or the TC-APC system loses power, the heartbeat watchdog times out and control reverts to the predefined fallback setpoints, with bumpless transfer.
- Switching it off. One action at the panel, or the loop goes to manual. No explanation required.
- The logic you commissioned. Not modified. TC-APC writes setpoints, and only setpoints.
Outside India
Your country, our engineering.
You own the client and the site work in your country. We customize and tune TC-APC to the process from India. That work is done offsite for every plant, so the distance changes less than you would expect.
Proof
Deployed, validated, and written down.
Deployed and validated
Fourteen carbonation towers at Saurashtra Chemicals
A division of Nirma Ltd, Porbandar. Validated over six months of plant operation.
Published
Chemical Weekly, 14 October 2025
Optimisation of chemical processes using hybrid technology, artificial intelligence and process knowledge. The approach, set out as a special report.
The group
An engineering group of IIT Bombay alumni
The engines behind TC-APC were built within the group.
Its associates include a Fellow of the Indian National Academy of Engineering who designed control systems for ISRO's launch vehicles.
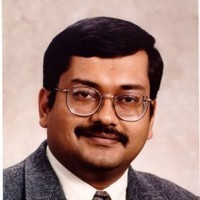 Chief Scientific Advisor
Prof. Pratim Biswas
Member, US National Academy of Engineering; former Dean of Engineering, University of Miami.
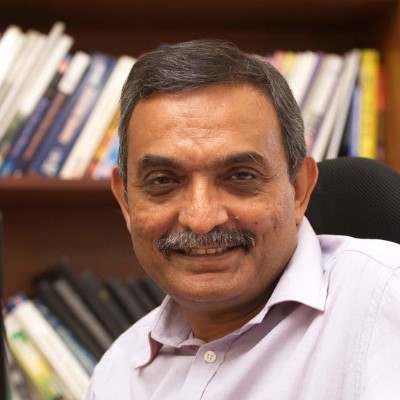 Chief Strategy Advisor
Prof. Janat Shah
Founding Director, IIM Udaipur; for two decades Professor of Operations Management, IIM Bangalore.
When your client asks who advises us on the science, the answer is a Member of the US National Academy of Engineering and former Dean of Engineering, University of Miami, whose industrial record includes the Paint to Power project with Chrysler and Ameren.
The mark
Find the optimum. Hold it while it moves.
The curve is a yield or selectivity response. The amber point is the optimum, and the dashed drop is where it sits on the operating axis.
The second half of the line is the part that matters. Finding an optimum is a study, and studies end up in drawers. Holding one while the feed, the fouling, the weather and the wear keep moving it is a control problem, and that is the work.
Contact
Become a TC-APC Solution Partner.
Start with a conversation: what TC-APC is, where it has run, and whether it fits the plants you serve. The plant can come later.
Talk to IIT Bombay engineers Call +91 94230 07004Monday to Saturday, 9:00 to 19:00 IST projects@yielddynamics.in